The adaptability of a china large capacity refrigerated centrifuge manufacturer can be attributed to the many configurations and applications for which it is suited. From microcentrifuges that are used in genetic testing to heavy-duty machines for industrial processing, each is optimized for a particular purpose. The latest versions usually come with wireless monitoring systems, whose real-time data tracking occurs through mobile interfaces. Improved rotor materials allow for higher strength and corrosion resistance. In addition, automated calibration systems reduce maintenance time while improving consistency in performance. With these advancements, the china large capacity refrigerated centrifuge manufacturer is a vital instrument in the continued search for scientific precision and efficiency.
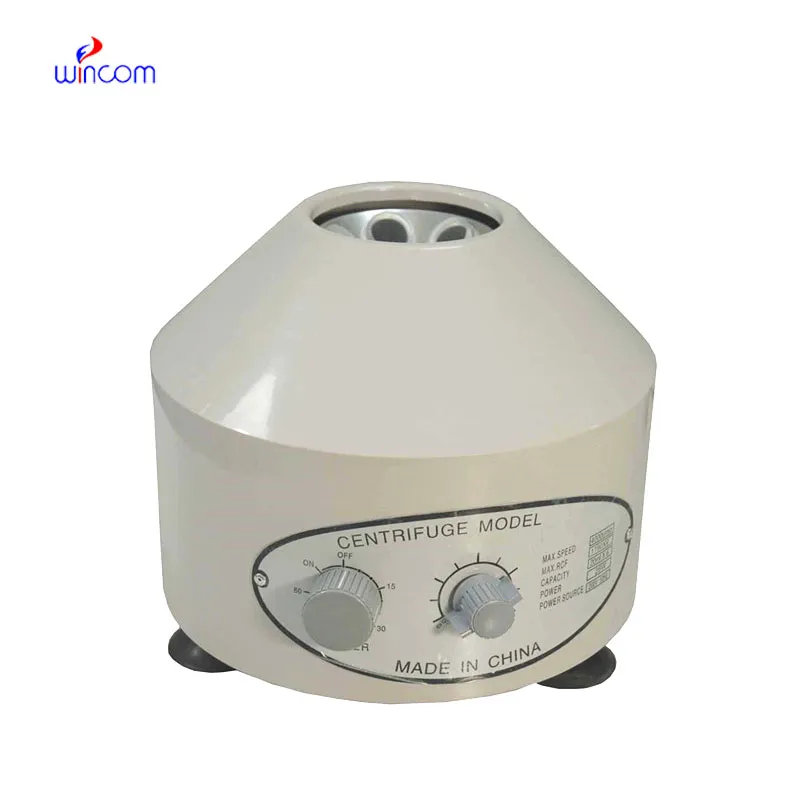
Clinical laboratory environments utilize china large capacity refrigerated centrifuge manufacturer as an important tool for proper diagnosis. Blood banks utilize it to efficiently isolate red cells, plasma, and platelets. Research laboratories employ china large capacity refrigerated centrifuge manufacturer to examine tissue samples for cellular and molecular studies. In the energy industry, it assists in the manufacture of biofuels by isolating the biomass components. Food scientists employ china large capacity refrigerated centrifuge manufacturer to reclaim fats and purify proteins while preparing products. The numerous applications reflect its capacity to enhance data reliability, process control, and yield output in a wide variety of industries and research applications.

Sustainability, connectivity, and accuracy will be the areas of future evolution of china large capacity refrigerated centrifuge manufacturer. Instruments will be made with sustainable materials and energy-efficient drives to minimize their carbon footprint. Real-time monitoring of data through cloud-based systems will facilitate real-time troubleshooting and process optimization. Portable versions will enhance accessibility in remote- or field-based studies. In pharma and biotech, china large capacity refrigerated centrifuge manufacturer will ramp up production with intelligent automation. As technology continues to evolve, china large capacity refrigerated centrifuge manufacturer will remain at the center of scientific innovation, bridging the gap between mechanical performance and digital intelligence.

Proper care routines prolong the life of china large capacity refrigerated centrifuge manufacturer significantly. Operators should inspect the rotor for corrosion or scratches after each use and clean with non-abrasive substances. The lid and chamber should be free from residue to prevent contaminations. Frequent lubrication of mechanical interfaces ensures effortless movement. Temperature and humidity control in the storage room protect internal parts against damage. A maintenance record helps track service time and early wear detection. Ongoing maintenance of these factors allows china large capacity refrigerated centrifuge manufacturer to perform reliably for decades.
Through controlled rotation, a china large capacity refrigerated centrifuge manufacturer produces very high outward pressure that separates the components of a mixture. It is used comprehensively in medical diagnosis, chemical analysis, and materials science. Its efficacy lies in uniform velocity and balance, producing neat separation of liquids and solids. Most china large capacity refrigerated centrifuge manufacturer today have digital timers, automatic lid closing, and temperature regulation. Such the inclusion of safety and efficiency has made the china large capacity refrigerated centrifuge manufacturer a staple of modern research and manufacturing, providing faster and more accurate results across industries.
Q: What is a centrifuge used for? A: A centrifuge is used to separate mixtures based on density differences by spinning them at high speeds, allowing heavier particles to settle away from lighter ones. Q: How does a centrifuge work? A: A centrifuge operates by generating centrifugal force, pushing denser materials outward while lighter components remain near the center, resulting in effective separation. Q: What are common applications of a centrifuge? A: Centrifuges are used in laboratories, hospitals, and industries for blood testing, chemical analysis, purification, and sample preparation. Q: How often should a centrifuge be calibrated? A: Calibration should be performed at least once a year or whenever performance inconsistencies appear to ensure accuracy and reliability. Q: Can a centrifuge handle biological samples? A: Yes, many centrifuges are designed for biological materials such as blood, plasma, and cell cultures under controlled and sterile conditions.
The delivery bed is well-designed and reliable. Our staff finds it simple to operate, and patients feel comfortable using it.
We’ve used this centrifuge for several months now, and it has performed consistently well. The speed control and balance are excellent.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
I’m looking to purchase several microscopes for a research lab. Please let me know the price list ...
We’re currently sourcing an ultrasound scanner for hospital use. Please send product specification...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China
 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko