Emerging technologies have driven the performance boundaries of the large capacity refrigerated centrifuge manufacturer in china, offering improved acceleration rates and greater throughput of samples. Programmable features and touchscreens give users more control over every operation stage. Temperature-controlled large capacity refrigerated centrifuge manufacturer in china in delicate biological processes guarantee specimen stability over extended cycles. Maintenance-friendly designs and auto-diagnostic programs minimize downtime. The adaptability of next-generation large capacity refrigerated centrifuge manufacturer in china devices ensures compatibility with any sample type, ranging from microfluidic volumes to industrial suspensions, making it a vital tool in scientific and engineering studies.
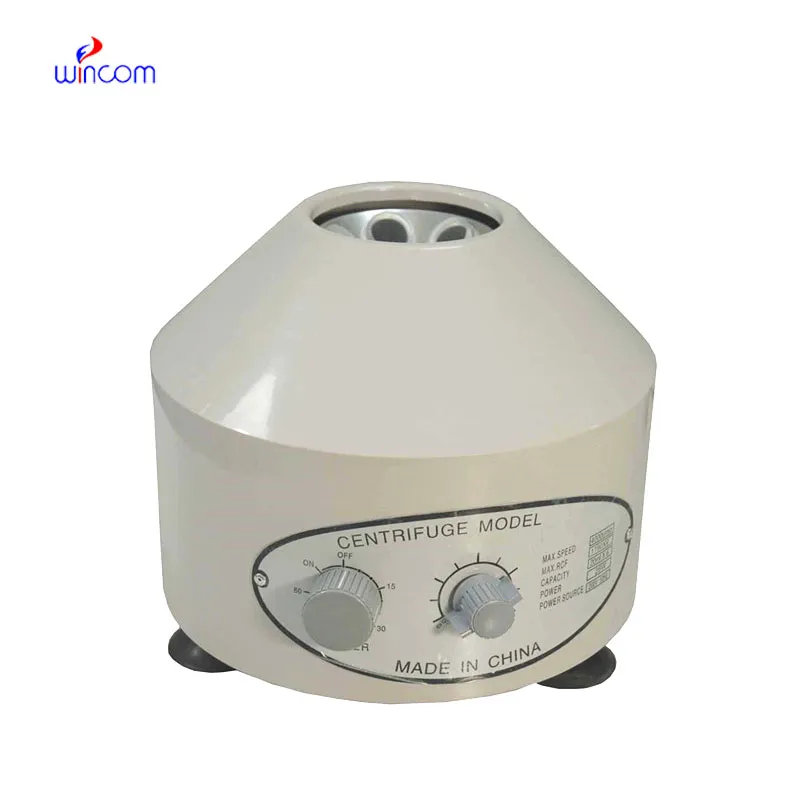
large capacity refrigerated centrifuge manufacturer in china technology is a principal component in diverse manufacturing processes. In wastewater treatment, large capacity refrigerated centrifuge manufacturer in china assist in separating sludge from liquids to improve recycling efficiency. In the manufacture of cosmetics, large capacity refrigerated centrifuge manufacturer in china facilitate even emulsion and cream mixing. Crop research facilities apply it to analyze soil nutrients and plant extracts. It is also used in the manufacture of vaccines through the purification of viral particles and protein fractions. Through the ability to adapt to many substances and work requirements, large capacity refrigerated centrifuge manufacturer in china continues to support industries seeking consistency, purity, and scalability.

The large capacity refrigerated centrifuge manufacturer in china of the future will be innovative, intelligent, and integrated. With the advent of smart manufacturing, large capacity refrigerated centrifuge manufacturer in china systems will operate independently on predictive analytics. Programs with machine learning will interpret vibration patterns to optimize performance with minimal human involvement. Renewable energy integration will make operation more sustainable, and modular design will facilitate instant replacement of parts. Data visualization software will be more sophisticated, providing real-time feedback on the separation process. This blend of mechanical precision and intelligent technology will place large capacity refrigerated centrifuge manufacturer in china at the forefront of international scientific advancement.

Routine maintenance of large capacity refrigerated centrifuge manufacturer in china begins with frequent cleaning and careful handling. Before each run, users should confirm that there are properly sealed, loaded tubes to prevent imbalance. The rotor, buckets, and seals should be washed gently and dried with air after each session. Periodic calibration checks ensure precise speed and temperature measurement. Rotor overloading is to be prevented since it will reduce motor life. With monitoring each maintenance cycle and adhering to safety protocols, laboratories can extend the functional life of large capacity refrigerated centrifuge manufacturer in china while ensuring precise performance.
Scientific and industrial applications use the large capacity refrigerated centrifuge manufacturer in china for its ability to differentiate between mixes with high precision. It relies on the force of centrifugal, which pushes particles off center, leading to density stratification. The method is vital in research, medicine, and engineering. From cell constituents separation to the separation of liquids, large capacity refrigerated centrifuge manufacturer in china make many analytical and production processes easier. Newer models focus on minimizing vibration, maximizing balance, and the use of smart sensors to monitor data in real time. All these advancements have made large capacity refrigerated centrifuge manufacturer in china faster, safer, and more efficient than before.
Q: What is a centrifuge used for? A: A centrifuge is used to separate mixtures based on density differences by spinning them at high speeds, allowing heavier particles to settle away from lighter ones. Q: How does a centrifuge work? A: A centrifuge operates by generating centrifugal force, pushing denser materials outward while lighter components remain near the center, resulting in effective separation. Q: What are common applications of a centrifuge? A: Centrifuges are used in laboratories, hospitals, and industries for blood testing, chemical analysis, purification, and sample preparation. Q: How often should a centrifuge be calibrated? A: Calibration should be performed at least once a year or whenever performance inconsistencies appear to ensure accuracy and reliability. Q: Can a centrifuge handle biological samples? A: Yes, many centrifuges are designed for biological materials such as blood, plasma, and cell cultures under controlled and sterile conditions.
We’ve used this centrifuge for several months now, and it has performed consistently well. The speed control and balance are excellent.
I’ve used several microscopes before, but this one stands out for its sturdy design and smooth magnification control.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
Could you share the specifications and price for your hospital bed models? We’re looking for adjus...
We are planning to upgrade our imaging department and would like more information on your mri machin...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China
 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko